
Dual-Pressure Instrument Air System with Booster Compressors
Central Air Equipment (CAE) engineered a dual-pressure instrument air system for an industrial facility requiring two distinct operating pressures. By combining commercially available rotary screw compressors with high-pressure booster compressors, CAE developed a cost-effective alternative to a custom high-pressure system, identifying approximately $65,000 in potential project savings.
Project Specifications
Application: Dual-Pressure Instrument Air System
Low-Pressure Air: 50 SCFM at 80 PSIG
Low-Pressure Air Quality: -40°C Pressure Dew Point
Medium-Pressure Air: 185 SCFM at 215.5 PSIG
Medium-Pressure Air Quality: +5°C Pressure Dew Point
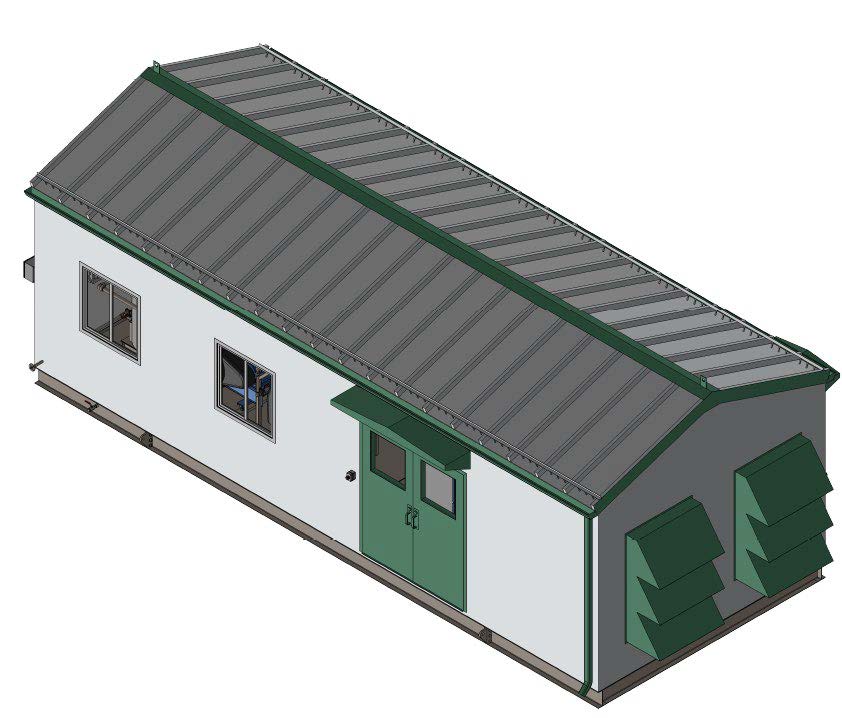
Configuration: Turnkey Building Package with Booster Compressors
The Challenge
The original design proposed using high-pressure electric compressors to supply both pressure requirements, with a downstream regulator reducing pressure for the low-pressure instrument air system.
However, maintaining a consistent 215.5 PSIG at the package outlet would require compressors capable of operating at approximately 235 PSIG to accommodate pressure fluctuations and losses through the air treatment equipment.
Rotary screw compressors suited to this pressure and flow range are difficult to source, making a custom-engineered system a potentially expensive solution.
CAE’s Solution
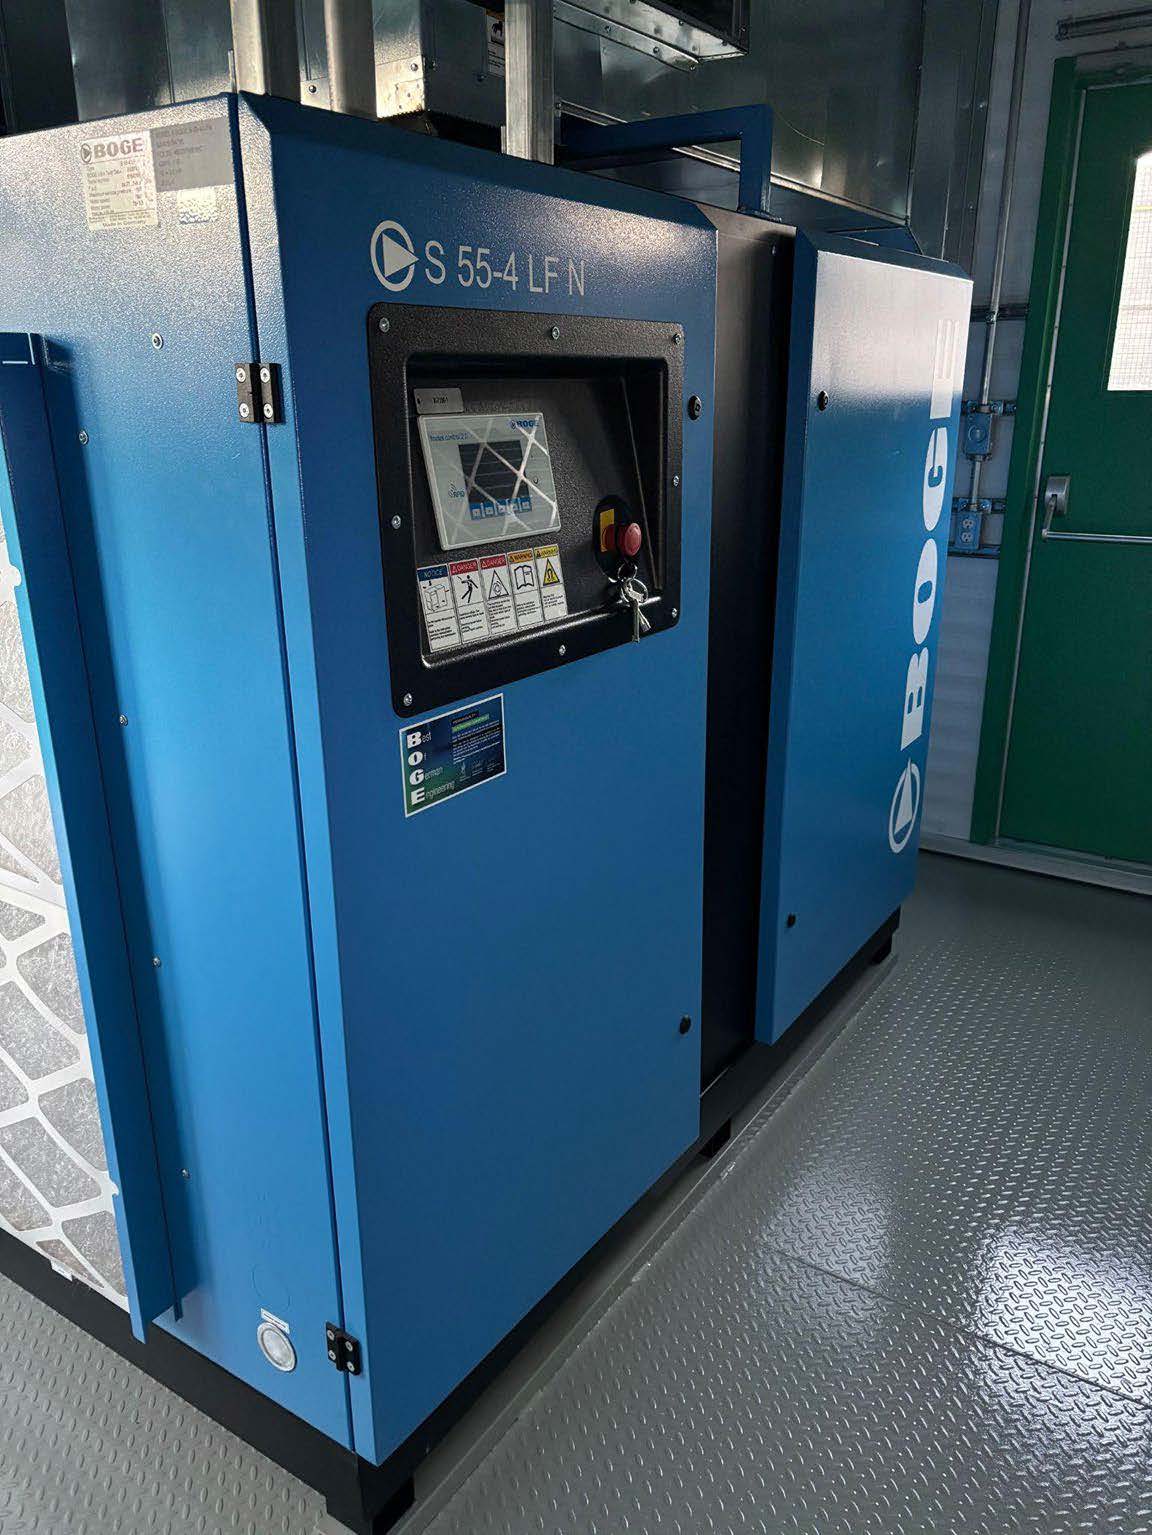
Rather than designing the entire compressed air system around the higher pressure requirement, CAE proposed using commercially available BOGE rotary screw compressors to supply low-pressure instrument air and feed a separate high-pressure booster system.
The booster compressors would increase pressure only where needed, eliminating the need for specialized high-pressure compressors to serve the entire system.
This configuration offered approximately $65,000 in estimated savings compared with the custom-engineered high-pressure alternative.
Equipment & System Configuration
The turnkey package included:
- Air Compressors: Two BOGE S55-4LF 75 HP direct-drive, variable-speed rotary screw compressors supplying low-pressure instrument air and booster feed air.
- Wet Air Storage: One common 240 USG wet air receiver sized for dryer purge air demand.
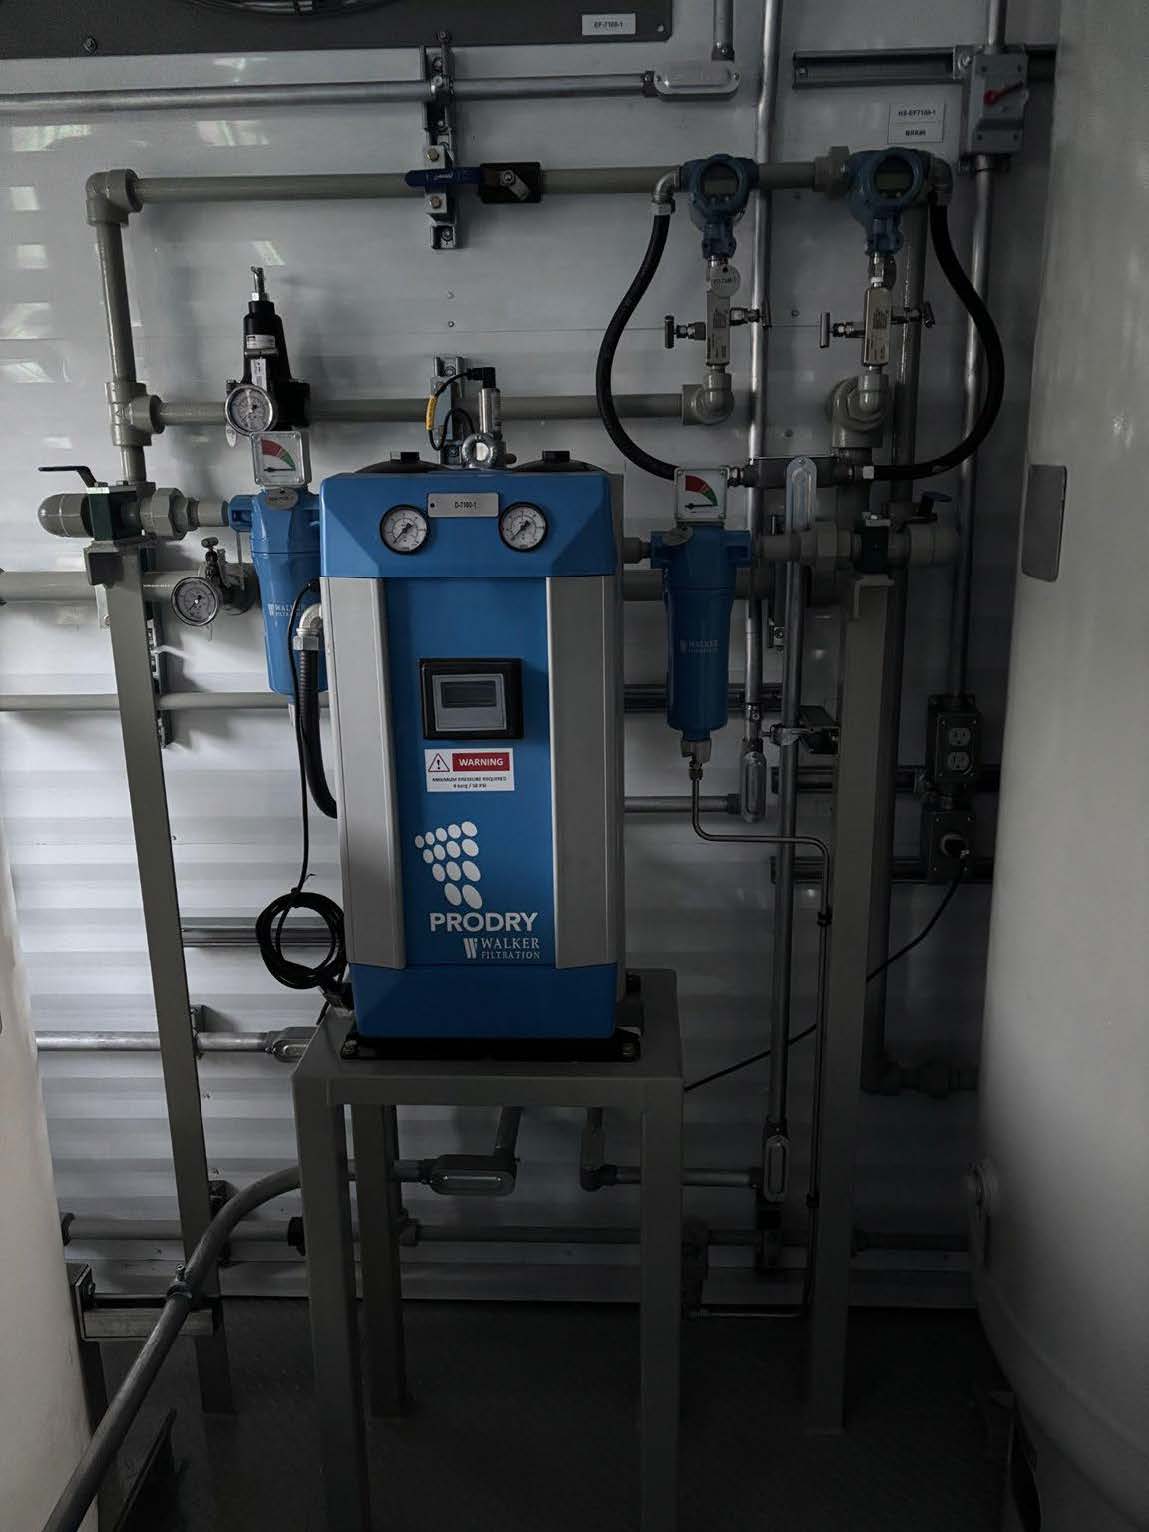
- Instrument Air Treatment: Walker PD0056-DMC modular heatless desiccant dryer with dew point control, sized for 100% of one compressor’s capacity and delivering a -40°C pressure dew point.
- Booster Feed Air Treatment: ATS DGU-350 refrigerated air dryer delivering a +3°C to +5°C pressure dew point, with pre-filtration and after-filtration.
- Air Storage: Two 400 USG receivers, one for low-pressure instrument air and one for booster feed air.
- High-Pressure Boosting: Three BOGE SRHV 470-10 booster compressors operating in parallel, with approximately 70% redundancy and associated filtration.
- Condensate Management: One 100 Imperial gallon collection tank for capturing and storing contaminated condensate.
The Result
CAE developed a dual-pressure compressed air package that addressed both operating requirements without relying on specialized high-pressure primary compressors.
By combining standard rotary screw compressors with dedicated booster technology, CAE provided a more practical equipment configuration while reducing projected system costs by approximately $65,000.
Need a Custom Compressed Air System?
Whether your application requires multiple operating pressures, specialized air treatment, or a complete turnkey package, CAE can help evaluate your requirements and engineer a solution that fits your operation.